Lines
Spi Bay
Spi Bay sits straight after stencil printing, where solder paste deposits are measured before components reach the placement heads. South African electronics teams use SPI to catch insufficient paste, bridging, offset and smear on defined board builds.
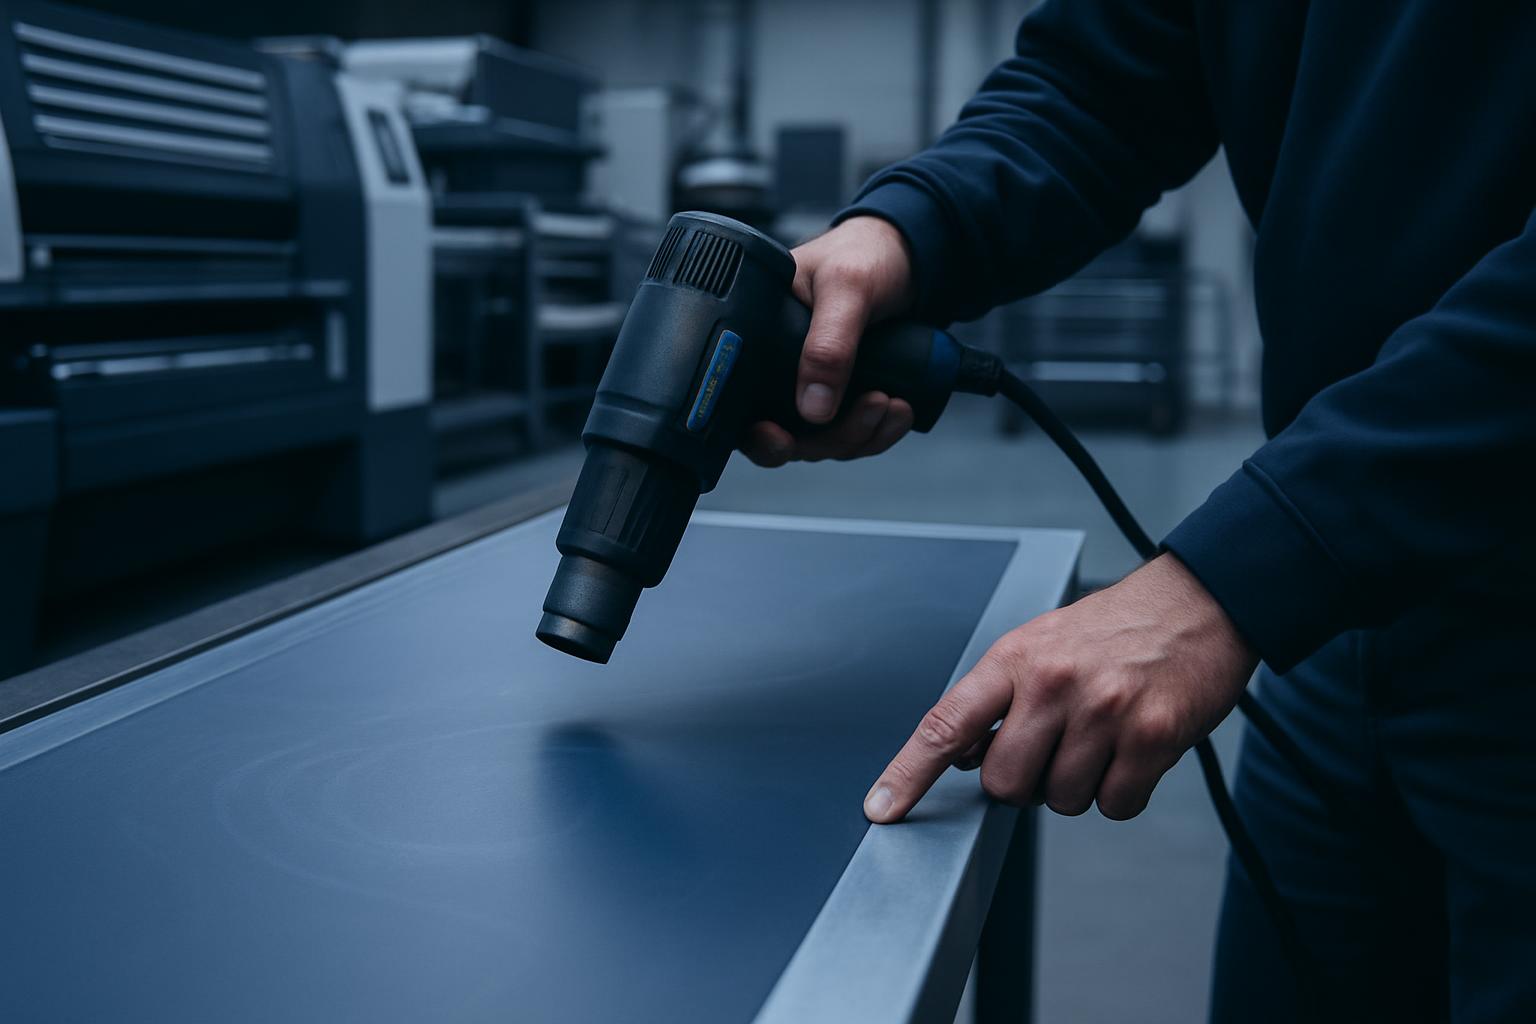
Paste inspection between print and placement
SPI is the stage in an SMT line where paste print quality is checked before placement starts. It is written for electronics teams in South Africa reviewing how inspection fits between stencil printing and pick-and-place. Use it when the board process is already defined and the focus is inspection on the line.
On this station, the board stops for a check on paste height, area and volume against the print program. Fine pitch pads, QFN ground patterns and small passive sites need tighter attention, especially when the stencil, squeegee pressure or understencil wipe interval has changed. In Gauteng dust and coastal humidity alike, print consistency can shift during the day, so SPI results need to be read with the line conditions in mind.
Capture the first inspected board after print settings are locked, then compare later results to that baseline rather than guessing from memory. A clear defect image at Spi Bay helps the printer operator trace whether the fault came from aperture release, board support, alignment or paste condition. That record is useful when a stop-start shift or power interruption breaks the normal rhythm of the line.
Checks that matter at Spi Bay
Use Spi Bay to decide whether the print is fit to feed the pick-and-place process, not only to collect pass data. The useful output is a short action list for the printer and the next article check, with thresholds that suit the actual pad geometry on the board. One stable print window on production boards counts more than a screen full of unused measurements.
Link Spi Bay findings to the printer setup and the next oven review before changing several variables at once. Confirm board orientation, fiducial read quality and defect limits before the run continues to placement. SMT line enquiries should name the board type, the placement volume and the machines already on the line.
- Paste volume checked before placement
- First article stored as baseline image
- Defect images attached to line notes
South African line conditions at SPI
At many South African sites, Spi Bay has to work around mixed board batches, utility interruptions and older printer platforms still doing daily production. A false fail rate wastes time, but loose tolerances allow bad prints to move downstream into expensive rework. Teams running from Johannesburg, Durban, Cape Town and smaller industrial areas usually need settings that reflect actual factory conditions rather than lab assumptions.
Coastal air can shorten the comfortable exposure window for solder paste once jars are opened and brought to line temperature. Inland dust can affect conveyors, sensors and camera windows, so cleaning discipline matters if the machine starts flagging random defects. Where generators or load-shedding disturb throughput, save the first-pass records early instead of waiting until end of shift.
Operated by Astros Marketing (Pty) Ltd from 2 Makro Place, Sunnyrock 1401.
Information worth sending for Spi Bay
Send the board type, paste brand, stencil thickness and the defect pattern seen at inspection. Add whether the issue appears on one area only or across the panel.
Log Spi Bay results on the same production run as the printer adjustments and reflow profile reference. Keep them with a project record and a quality sheet when the buyer or process engineer needs traceable line evidence.
What our SMT Line customers say
Verified Google reviews